About Us
One - stop Printed circuit board assembly Solution provider Keep Best PCB Assembly Co., Ltd serves many well-known brand customers in industrial control, security, medical, Internet of Things, automotive, artificial intelligence, smart home, power and communications industries at home and abroad. The company continues to be customer-centric, improves the level of digital intelligence, and is committed to meeting continued high-quality customer needs.
Quick PCBA Quote
Share your files and build requirements
PCBA Inspection and Testing: Build a Plan Around Coverage
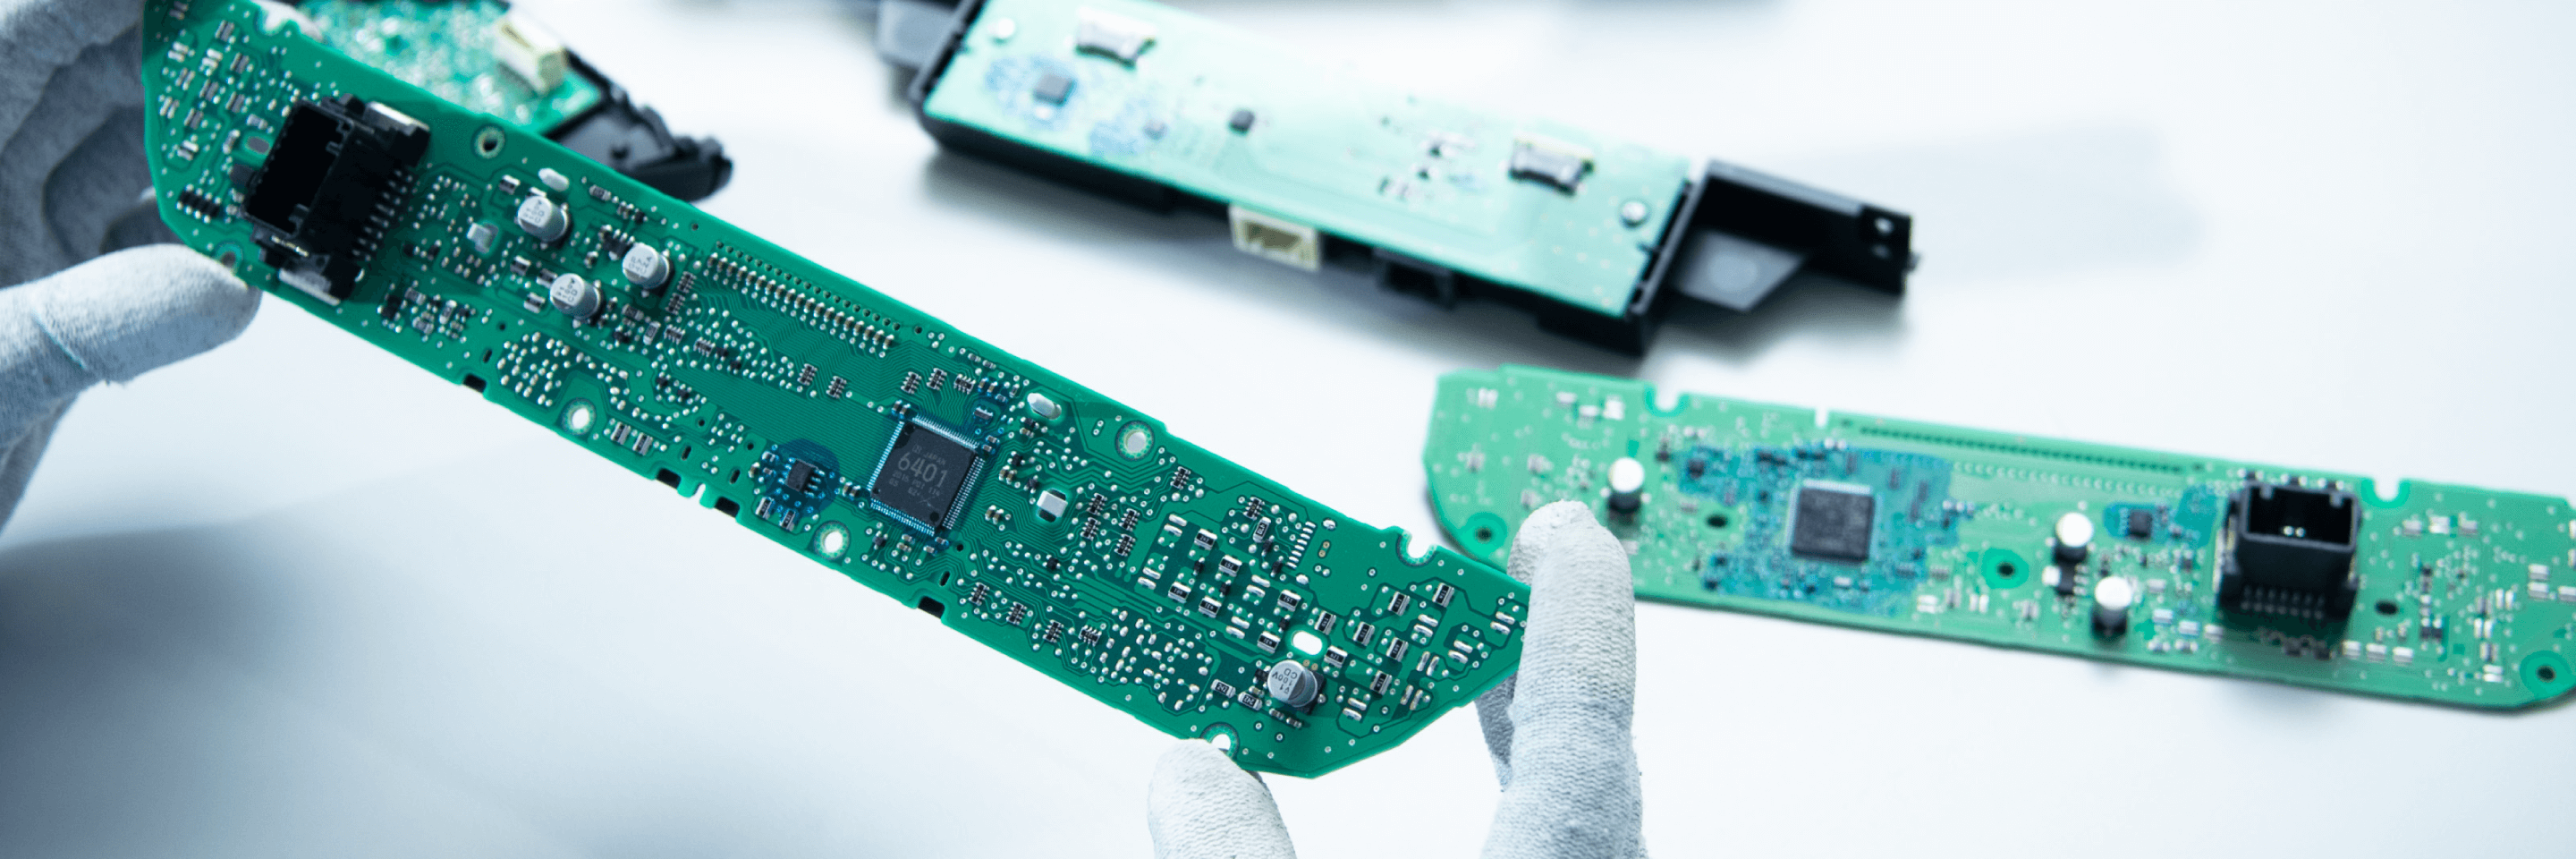
Assembly illustration; confirm the executing site and accepted scope for your project.
-
KeepBestPcba
-
Published
Updated
-
Views ()
PCBA Inspection and Testing: Build a Plan Around Coverage
Define PCBA inspection and test coverage. Compare the role of visual checks, AOI, X-ray, electrical tests and customer-specific functional testing.
PCBA inspection and testing should be selected according to the defects and product requirements that need to be checked. Solder paste inspection, automated optical inspection, X-ray inspection, in-circuit testing and functional testing examine different features. No method, or phrase such as “fully tested,” defines complete coverage without a project-specific test plan.
Start with a list of important failure modes and required functions. For each one, identify the method, access, acceptance limit, inspection or test frequency and record. This makes omissions visible before fixtures, software and production instructions are committed.
Understand what each method contributes
| Method | Typical purpose | Important boundary | Information needed to plan it |
|---|---|---|---|
| Solder paste inspection (SPI) | Examine printed paste deposits before component placement | It does not establish final solder-joint integrity or product operation | Paste-related features, program, limits and disposition rules |
| Automated optical inspection (AOI) | Examine visible assembly features such as component presence, placement and accessible solder features | Optical visibility and the inspection program limit coverage | Board data, component library, inspectable features and review rules |
| X-ray inspection | Examine selected features hidden from optical view, including joints beneath some packages | Image interpretation, geometry and technique matter; it is not a functional test | Target joints, required image method, acceptance criteria and sampling or full-unit scope |
| In-circuit test (ICT) | Check accessible electrical characteristics and connections using a defined program | Access, circuit interaction and program coverage constrain what can be measured | Netlist, test points, fixture, device models and limits |
| Functional test (FCT) | Exercise defined product functions under specified conditions | It checks the functions and conditions included in the procedure | Firmware, stimulus, loads, interfaces, fixtures, sequence and pass/fail limits |
Nordson's published SPI description includes measurements of paste height, area, volume and registration; its optical systems address visible assembly features. These are examples of inspection purposes, not evidence of equipment installed at a particular assembler. Nordson: Official inspection system descriptions.
Nordson also describes X-ray applications for hidden solder-joint defects. The suitability of an image technique for a particular package must be established; the name “X-ray” alone does not specify the views, analysis or coverage. Nordson: AXI applications.
Keysight distinguishes ICT electrical checks from functional testing of overall behavior and describes fixture access to test points. A practical plan still needs to identify inaccessible nodes and untested functions rather than assuming every circuit feature is covered. Keysight: In-circuit test systems and FAQ.
Keep bare-board testing separate
Bare-board electrical testing checks the unpopulated board against its specified connectivity requirements. It does not demonstrate correct component placement, soldering, firmware or assembled product behavior. An RFQ should state the requirements for bare-board acceptance and for assembly acceptance separately.
Similarly, a visual pass does not establish that the correct firmware was loaded or that a sensor reads accurately. A functional pass may not identify an assembly defect that does not affect the functions exercised by the test. The plan should explain how the selected methods work together and what remains outside coverage.
Create a risk-to-coverage worksheet
For each important risk or requirement, record:
- The requirement or potential failure, with its source in the product specification or manufacturing review.
- The feature, reference designator, net or function being checked.
- The chosen inspection or test method and the stage at which it runs.
- The required access, fixture, software and operator action.
- The acceptance limit and the person authorized to approve it.
- Whether the check applies to every unit or a defined sample, and why.
- The retained result, unit or lot identifier, and failure disposition.
- Any gap, compensating control or additional validation required.
Use this worksheet to discuss coverage rather than collecting equipment names. The appropriate method depends on the actual board, its risks and the supplier's confirmed process. A machine list does not establish that a specific inspection program exists for your product.
Define functional tests with measurable outcomes
A functional procedure should describe the supply conditions, firmware revision, test sequence, input stimuli, loads and expected outputs. Replace “works normally” with an approved measurable limit or a clearly defined observable result.
Identify how calibration or measurement uncertainty affects pass/fail decisions where relevant. State whether the procedure is intended to check assembly quality, product performance, a safety requirement or another objective. A manufacturing functional test does not automatically replace design qualification or product regulatory testing.
Consider how a failed unit is handled. Define what may be repeated, when a retest requires investigation, how rework is recorded and who can release the unit. Preserve the original failure result where records are required; repeatedly testing until a pass can conceal intermittent problems.
Validate the program before using it for release
Check that the approved program identifies the correct product variant and configuration. Evaluate repeatability, fixture contact and relevant known failure conditions where practical. Document the limits and coverage rationale, then control subsequent changes to software, firmware, fixtures and instructions.
When a fixture or test program changes, decide which checks need repeating. A minor software edit can affect a limit, a skipped step or the identification stored with a result. The product and test owners should determine the revalidation scope.
Specify frequency and records explicitly
“Every unit tested” means every unit receives the defined test; it does not mean every possible defect is detected. Sampling should identify the population, selection rule, acceptance decision and response to a failure. Do not describe a sampled check as a complete unit-by-unit check.
Ask which records can be supplied: inspection dispositions, measured values, firmware identity, unit identifiers, rework history or shipment release records. Retention duration and customer access should be agreed rather than inferred from a general traceability claim.
A test plan is also a quotation input. Fixture development, program creation, debugging and test cycle time can affect cost and schedule. Agree those activities before production, especially when the customer has not yet provided a functional procedure.
Discuss coverage for your board
Use the finished product test page and quality assurance page to frame the requirements you need reviewed. Contact KeepBest with the board revision, important functions, packages of concern and available test information. The inspection methods, equipment, coverage, frequency and records must be confirmed for the specific project.
Recent Post
Ask a PCBA question
Your question is sent privately to our team. Required fields are marked *.
Quick PCBA Quote
Share your files and build requirements